
What Is DFM for Injection Molding?
DFM for injection molding converts product requirements into approved decisions before steel machining starts. Rule lists flag thin walls or weak draft but cannot record gate-mark acceptance, shrinkage assumptions, or release evidence. Useful DFM connects geometry, material, mold concept, validation, cost, and revision ownership.
1. What Does DFM for Injection Molding Need to Decide?
DFM should decide whether a defined part can be molded, measured, assembled, and validated under agreed conditions. That decision needs controlled product data plus named owners for risks, changes, and acceptance.
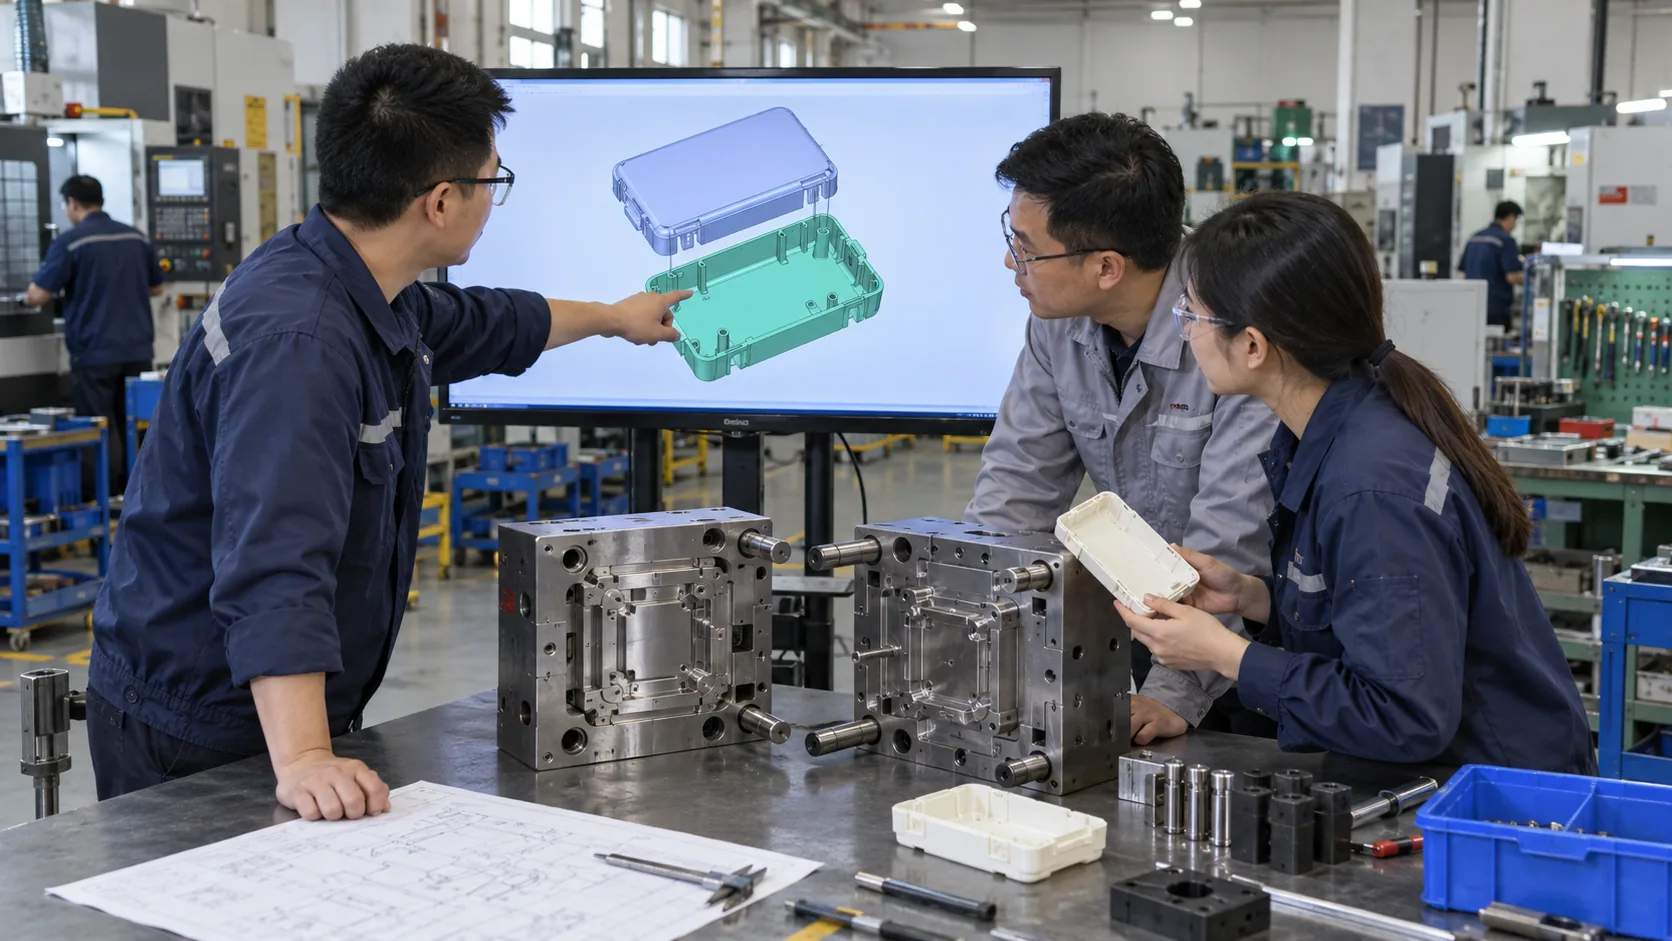
Treat DFM as a decision record. Each finding should connect a feature with its molding mechanism, likely consequence, proposed response, owner, due date, and approval status. “Add draft” becomes useful only after teams identify a surface, release direction, texture need, accepted angle, and model revision.
A complete workflow should decide:
- Which product requirements remain fixed
- Which features may change before tooling
- Which risks move into mold design or processing
- Which evidence closes each open item
- Who authorizes steel release
DFM sets boundaries and handoffs for detailed mold design, analysis, trials, and production qualification.
Action recommendation: Define required DFM outputs and signatories in your RFQ before suppliers begin reviewing CAD.
Which outputs make a DFM review actionable?
| Workflow output | Question answered | Owner | Release evidence |
|---|---|---|---|
| Input register | What data controlled this review? | Project lead | Revision list |
| Issue register | Which risks need decisions? | Product and tooling teams | Closed dispositions |
| Mold concept | How will part be formed and released? | Tooling engineer | Approved concept drawing |
| Validation plan | How will success be judged? | Quality and product teams | Signed acceptance matrix |
2. Which Inputs Must Be Ready Before a DFM Review?
Good reviews begin with stable inputs. Controlled 3D CAD defines geometry, while a 2D drawing states dimensions, tolerances, datums, material, finish, and notes. Neither file usually explains demand, assembly loads, cosmetic zones, target press, or validation method. Those facts change mold decisions.
Missing data should stay visible. Suppliers should label assumptions instead of silently choosing a resin, shrinkage value, texture, cavity count, or acceptance standard. An assumption register lets buyers approve, correct, or defer each point without losing its effect on cost and steel.
Prepare these inputs:
- Native or neutral 3D CAD with revision identifier
- Controlled drawing plus critical-feature markings
- Exact resin grade, color, additives, and allowed alternatives
- Annual volume, ramp plan, program life, and service demand
- Mating parts, assembly sequence, loads, and test conditions
- Cosmetic boundaries, texture, gate, ejector, and parting-line limits
- Target machines, automation, mold standard, and receiving plant
- Required sample, inspection, capability, and approval records
For any unknown input, record its deadline and affected tool features.
Action recommendation: Refuse steel release when an unresolved input can change cavity geometry, shrinkage, gate position, or validation scope.
What should pass the input-readiness gate?
| Input group | Minimum content | Risk if missing | Gate result |
|---|---|---|---|
| Product definition | CAD, drawing, revision, datums | Conflicting geometry or inspection | Hold review scope |
| Material | Supplier, grade, color, filler | Wrong shrinkage or processing basis | Hold steel dimensions |
| Demand | Annual and peak needs | Wrong cavity and runner concept | Hold mold concept |
| Acceptance | Function, cosmetics, measurement | Trial dispute | Hold validation release |
3. What Should a Useful DFM Report Contain?
A useful report shows decisions in context. Begin with identifiers, file revisions, resin, demand, target machine, assumptions, participants, and date. Then organize an issue register by feature or risk. Each issue needs location, mechanism, consequence, options, owner, and status.
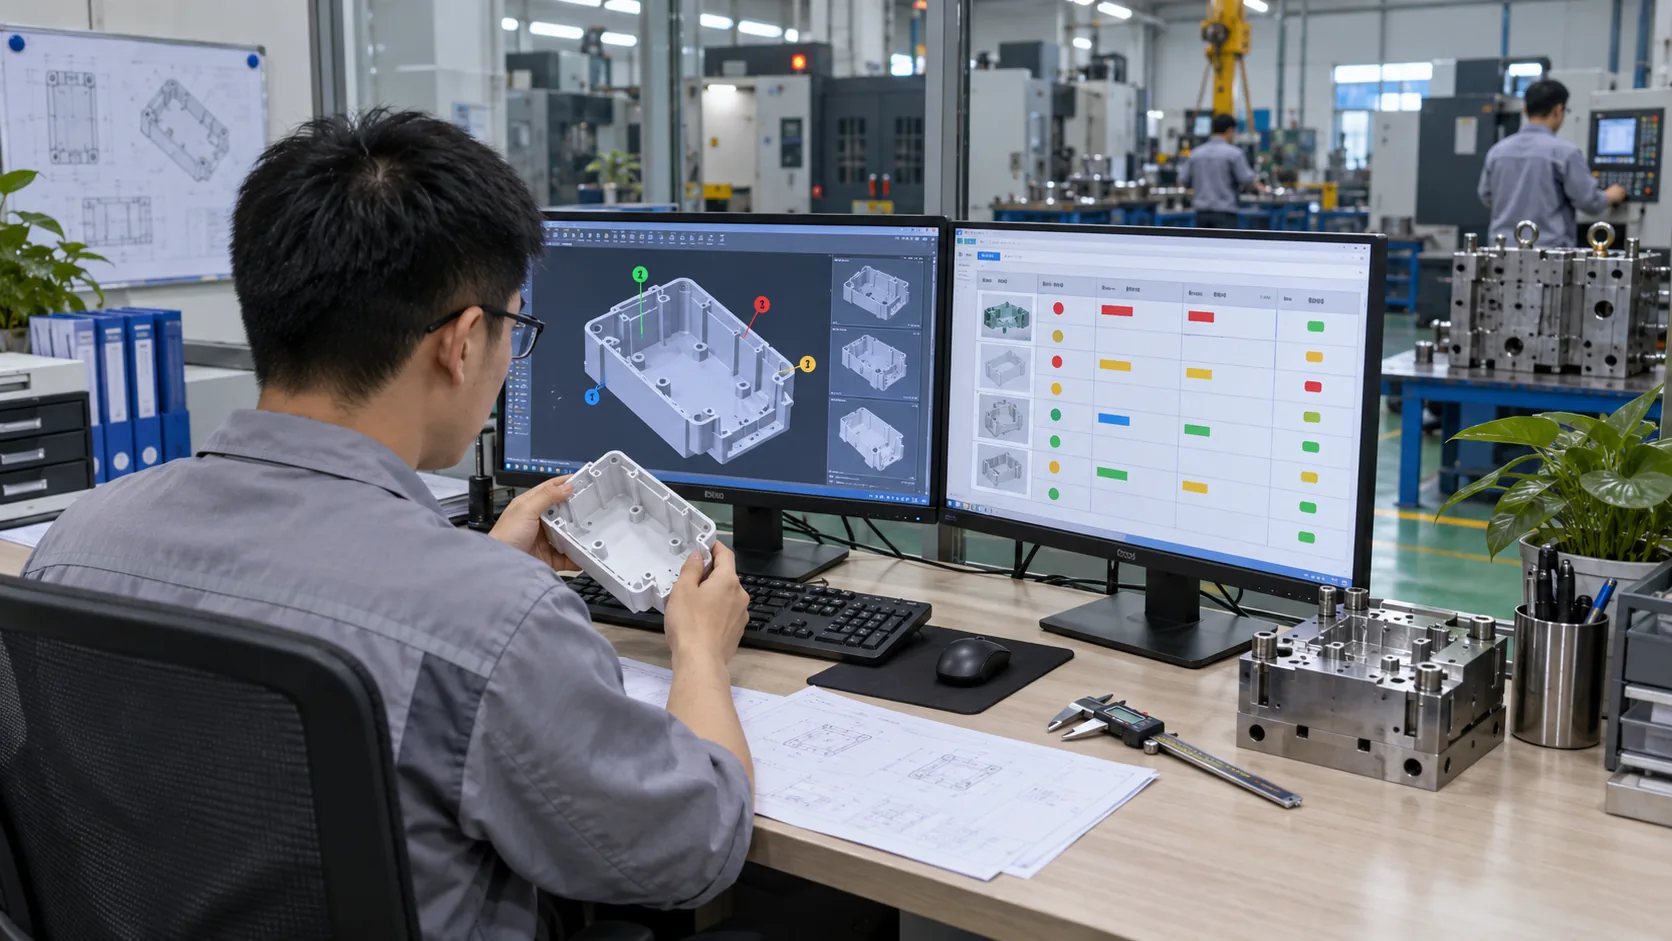
Screenshots need a paper trail. Every marked image should reference a CAD feature, drawing zone, or item number. Status choices should remain plain: open, accepted, revised, rejected, or transferred into another controlled plan. Avoid vague labels such as “please check” because no closure rule follows them.
Report contents should cover:
- Executive decision summary with open release blockers
- Controlled input and assumption register
- Parting, release direction, gate, runner, and ejection concept
- Geometry, tolerance, cosmetic, assembly, and material findings
- Analysis requests with stated assumptions
- Decision log, ownership, due dates, and approval history
- Validation plan plus engineering-change method
Keep commercial exclusions outside screenshots, yet link each cost effect with its issue number.
Action recommendation: Return reports that lack revision traceability or owner-based closure before approving a mold concept.
Which report fields prevent ambiguous closure?
| Report field | Required detail | Weak version | Closure test |
|---|---|---|---|
| Location | Feature ID and marked view | Unnumbered screenshot | Reviewer finds same feature |
| Mechanism | Molding or tooling cause | Generic risk label | Cause can be discussed |
| Disposition | Accepted response and revision | “Customer aware” | Decision has named owner |
| Evidence | Updated file, analysis, or test | Verbal agreement | Record can be retrieved |
4. How Should Geometry Decisions Be Reviewed and Closed?
Geometry review should follow molding and release paths. Trace melt through each thickness transition, then trace cooling, shrinkage, opening, actions, and ejection. This exposes interactions that isolated rules miss. A rib can improve stiffness while creating sink, trapped gas, or thin steel nearby.
Close features in their real neighborhoods. Review bosses with mating screws and supporting ribs. Review draft with texture, depth, and release direction. Review undercuts with assembly need, slide travel, shutoff, wear access, and possible redesign. Review tolerances with function, datum scheme, material, cavity layout, measurement method, and conditioning.
Geometry checks should include:
- Wall transitions, local mass, ribs, bosses, and radii
- Draft by surface, texture, depth, and ejection direction
- Undercuts, shutoffs, slides, lifters, and steel strength
- Parting lines, flash-sensitive edges, and cosmetic surfaces
- Gate vestige, weld-line location, venting, and ejection marks
- Assembly stack-up, datum logic, and functional tolerances
Each accepted risk should name a downstream control.
Action recommendation: Ask product engineering to approve visible marks and functional changes while tooling approves mold feasibility.
How should geometry items reach a decision?
| Geometry item | Mechanism to review | Possible disposition | Closure evidence |
|---|---|---|---|
| Thick boss base | Uneven cooling and sink | Core, thin, relocate, or accept | Revised section and visual limit |
| Textured wall | Release drag | Add draft or change texture | Surface callout approval |
| Undercut | Mechanical release | Slide, lifter, insert, or redesign | Approved mold action |
| Tight dimension | Shrinkage and measurement | Relax, control, or qualify | Functional rationale and method |
5. How Do Material and Tooling Decisions Stay Connected?
Material affects shrinkage, flow, heat, moisture, wear, venting, surface replication, and dimensions. Tooling affects those outcomes through gate, runner, cooling, steel, texture, cavity layout, and process window. Late material review leaves coupled choices open.
Lock exact grade assumptions early. “ABS” or “PC blend” rarely gives enough detail. Use supplier, grade, filler, color, recycled-content rule, flame requirement, and approved alternatives. When substitution remains possible, show which tool dimensions or validations need rechecking.
Link material with these tool decisions:
- Shrinkage basis and steel-safe dimensions
- Gate type, location, restriction, and vestige
- Runner choice plus allowed regrind
- Cooling layout and target mold temperature
- Venting, polishing, texture, and release
- Wear areas, replaceable inserts, and service access
- Cavity count and expected process balance
Data-sheet values often come from test specimens. Production behavior also reflects geometry, orientation, gate layout, cooling, and process settings.
Action recommendation: Put resin grade and shrinkage approval on mold-concept drawings rather than leaving them only in email.
Which linked decisions require joint approval?
| Material input | Tooling decision | Production risk | Joint approvers |
|---|---|---|---|
| Shrinkage behavior | Cavity steel size | Out-of-tolerance part | Product, tooling, material |
| Flow and shear response | Gate and runner | Fill or material damage | Process and tooling |
| Filler and abrasion | Gate insert and wear plan | Drift or repair burden | Tooling and maintenance |
| Surface and color | Polish, texture, venting | Cosmetic rejection | Product and quality |
6. When Should Analysis or Trials Support the Review?
Analysis earns its place when uncertainty can change design. Flow studies can compare gates, pressure, balance, weld lines, air traps, packing, cooling, and warpage tendencies. Results depend on geometry, mesh, resin data, assumptions, and scope.
Escalate uncertainty with a clear question. Ask whether one gate can fill a long thin region, whether cavities balance, or whether cooling differences threaten a datum. Define alternatives before running analysis. Then compare results against machine, appearance, function, and tooling constraints.
Evidence may include:
- Gate-location or filling comparison
- Pressure and clamp-demand estimate
- Cooling-circuit review or thermal study
- Warpage tendency with defined restraint and measurement basis
- Prototype, material coupon, or representative feature trial
- Supplier processing guidance for a selected grade
Simulation cannot approve an impossible gate mark or inaccessible cooling line. Engineering still closes physical constraints.
Action recommendation: Require each analysis request to state its decision, alternatives, inputs, acceptance rule, and report owner.
Which uncertainties deserve added evidence?
| Uncertainty | Useful evidence | Decision supported | Limit to record |
|---|---|---|---|
| Long or thin flow | Fill and pressure comparison | Gate count and location | Material and machine assumptions |
| Multi-cavity balance | Runner and cavity study | Feed-system concept | Modeled symmetry and tolerances |
| Uneven thermal mass | Cooling and warp study | Cooling or geometry change | Boundary conditions |
| New material-feature pair | Representative molding trial | Process feasibility | Prototype-tool differences |
7. Which Sign-Off Gates Belong Before Steel Is Cut?
Steel release should follow named gates with evidence and authority. What DFM should resolve before steel is cut adds broader tooling context. One “DFM approved” email hides which revision, mold concept, material, validation plan, and risks received approval. Separate gates simplify later changes.
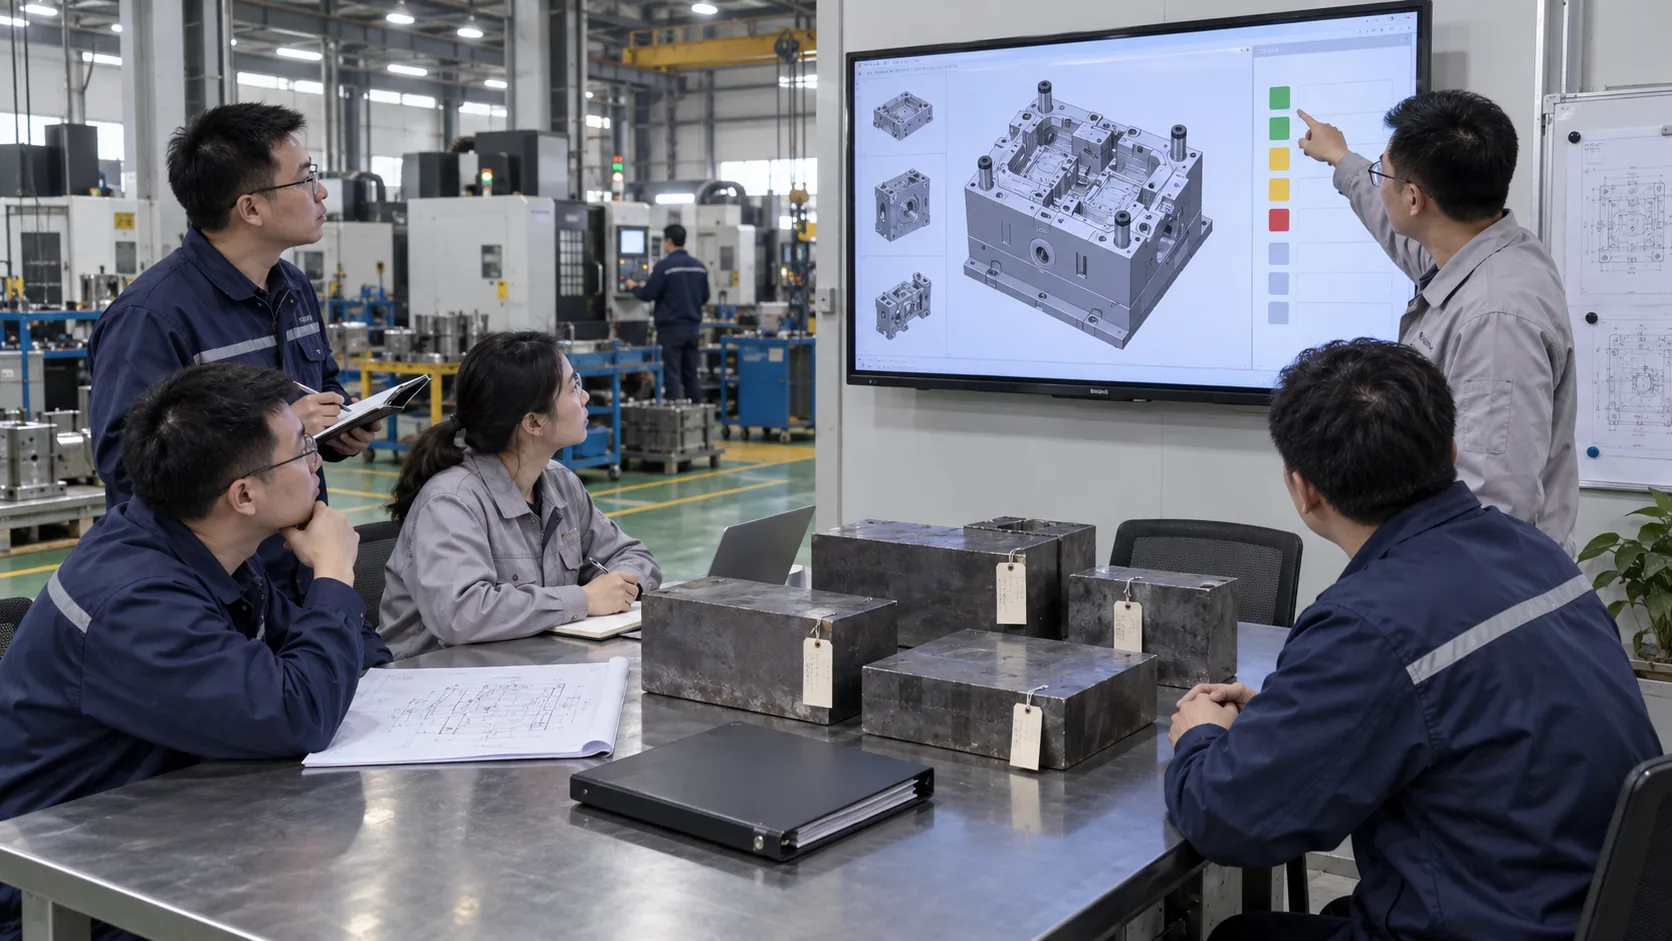
Release needs a stop rule. Classify open items as blocking, conditionally accepted, or downstream actions. Blocking items prevent any steel machining. Conditional items require named assumptions plus approved exposure. Downstream actions move into mold design, trial, or validation with owners and due dates.
Recommended gates include:
- Product-definition gate for CAD, drawing, material, and requirements
- DFM issue gate for closed geometry and appearance decisions
- Mold-concept gate for parting, gate, actions, cooling, and ejection
- Analysis gate for agreed high-risk findings
- Commercial gate for scope, exclusions, and change responsibility
- Steel-release gate for final revisions and signatures
Procurement confirms agreed commercial scope. Engineering approves product and mold decisions. Quality approves measurement and acceptance. Supplier roles sign technical commitments.
Action recommendation: Use a one-page release sheet that references detailed records without replacing them.
Who should sign each pre-tooling gate?
| Gate | Required evidence | Primary sign-off | Hold condition |
|---|---|---|---|
| Product definition | Controlled files and requirement list | Product engineering | Conflicting revisions |
| Mold concept | Approved layout and assumptions | Tooling engineering | Open gate or action choice |
| Validation | Measurement and trial plan | Quality and product teams | Undefined acceptance |
| Steel release | Closed blockers and priced scope | Buyer plus supplier leads | Unapproved change exposure |
8. How Should DFM Define Validation Before Tooling Starts?
Validation requirements shape mold design, samples, fixtures, process records, and timing. Define them during early DFM. A good-looking sample cannot prove dimensional, assembly, functional, or repeat-process requirements without planned checks.
Approval criteria belong beside design decisions. Critical dimensions need datums, method, conditioning, sample quantity, cavity identity, and timing. Cosmetic zones need viewing conditions and defect limits. Functional checks need mating components, fixtures, loads, and pass criteria. Process evidence needs machine, resin lot, drying, temperatures, pressures, cycle, and cavity tracking as appropriate.
Build a validation package from:
- Trial purpose and entry criteria
- Approved resin, color, machine, and mold condition
- Sample quantity by cavity and production interval
- Dimensional, cosmetic, assembly, and functional checks
- Process sheet plus material-handling record
- Issue log with correction and rerun evidence
- Conditions for pilot, capacity, or production release
Request records that support decisions. Paperwork cannot repair an undefined acceptance rule.
Action recommendation: Approve a validation matrix before machining any feature whose acceptance depends on a special gauge or test.
What evidence should a validation plan request?
| Evidence | Question answered | Defined during DFM | Release use |
|---|---|---|---|
| Trial process sheet | How were samples molded? | Required parameters and identifiers | Setup reference |
| Dimensional plan | What gets measured and how? | Features, datums, method, quantity | Engineering approval |
| Cosmetic standard | What appearance passes? | Zones, conditions, defect limits | Visual release |
| Issue closure | Did correction solve cause? | Owner, action, rerun rule | Tool and launch release |
9. How Should Engineering Changes Be Controlled After Approval?
Every post-approval change should identify origin, files, technical impact, cost, schedule, validation, and authorization. Update controlled CAD and drawings rather than one screenshot. Suppliers should identify steel already machined from an older revision.
Change control protects both sides. Customer revisions, supplier corrections, material substitutions, tool-detail changes, and process adjustments have different responsibilities. Label each change category clearly. A supplier-requested draft increase may affect appearance, while a customer-requested wall change may alter cooling, shrinkage, gate behavior, and quotation scope.
A change record should include:
- Unique change number and request origin
- Old and new file revisions
- Marked geometry or requirement difference
- Mold, material, process, inspection, cost, and timing impact
- Steel-safe or irreversible status
- Required analysis, trial, and reapproval
- Signatures plus implementation evidence
Keep superseded files accessible but clearly obsolete.
Action recommendation: Freeze machining whenever a pending revision affects cavity steel until authorized impact review finishes.
What should every engineering-change record show?
| Record field | Why it matters | Required decision | Closure evidence |
|---|---|---|---|
| Revision pair | Defines exact change | Accept correct baseline | Archived old and released new files |
| Impact review | Exposes downstream effects | Approve scope and exposure | Signed assessment |
| Steel status | Shows reversibility | Machine, hold, weld, or remake | Tooling confirmation |
| Revalidation | Protects approved functions | Repeat selected checks | Updated reports and samples |
10. What Should You Send With an RFQ or Pre-Tooling Package?
Send a controlled package so each supplier reviews the same production case. Include geometry, requirements, material, demand, mold standards, target plant, validation expectations, and requested DFM format. State that named gates control steel release and follow the DFM-to-mass-production workflow through tooling, trials, and production.
A complete package saves the right questions. It cannot remove engineering discussion, though it keeps that discussion focused on real tradeoffs.
Your package should contain:
- 3D CAD and controlled 2D drawing
- Revision history plus open design items
- Exact material and approved alternatives
- Annual demand, ramp, program life, and cavity preference
- Cosmetic map, assembly data, and critical characteristics
- Mold standard, target press, utilities, and receiving plant
- DFM report template or required issue fields
- Trial, inspection, function, and release expectations
- Change-control and steel-release authority
From a factory review standpoint, this package focuses discussion on geometry, tooling, and production evidence while changes remain manageable.
Action recommendation: Send one version-controlled package, collect written questions, close blocking items, and release steel only through named signatories.
Frequently Asked Questions
- Q1: Is DFM the same as mold design? No. DFM approves product and manufacturing decisions. Detailed mold design converts those approved boundaries into plates, inserts, mechanisms, cooling, feed systems, and service details.
- Q2: Who should approve a DFM report? Product engineering, tooling, quality, procurement, and supplier engineering should approve fields within their authority. One project lead should control final release status.
- Q3: Does every part need mold-flow simulation? No. Use analysis when uncertainty can change a gate, geometry, cavity, cooling, machine, or validation decision. State inputs and limitations.
- Q4: Can tooling start with open DFM items? Only when each item receives a non-blocking classification, named assumption, owner, deadline, and approved risk. Cavity-affecting uncertainty should hold steel.
- Q5: How should suppliers handle late CAD changes? Stop affected work, compare revisions, document tool and validation impacts, price authorized scope, then obtain reapproval before implementation.